Milk/Dairy and Sweets Processing
Hygienic Dairy Processing Plants
Tatar Advance Technology Pvt. Ltd. provides integrated dairy-processing solutions for milk reception, testing, chilling, standardisation, pasteurisation and packaging, along with facilities for producing value-added milk products.
Each plant is designed according to the daily milk-handling capacity, product mix, operating hours, packaging format, required shelf life, cleaning system and cold-chain requirements.
500–5,000
200–10,000
1000–10,000
10-50
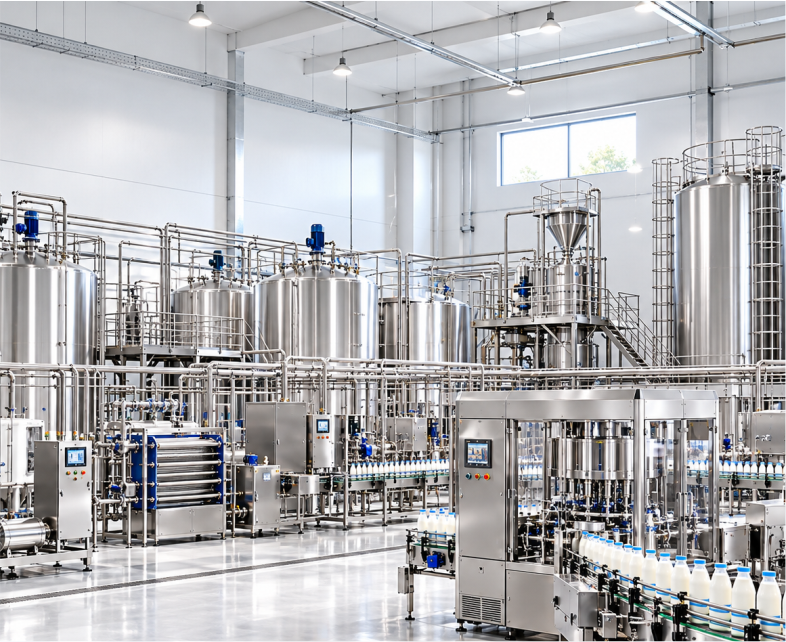
Complete Dairy Processing Workflow
A practical end-to-end line that can be configured around the required dairy product, capacity and packaging format.
1
Milk Reception and Chilling Section
A modern milk reception and chilling system designed for efficient milk collection, weighing, testing, filtration, and safe handling
2
Milk Processing Section
A comprehensive milk processing setup designed for clarification, cream separation, standardisation, pasteurisation, and homogenisation.
3
Pasteurised Milk Packing Section
An efficient packing system for hygienic filling, sealing, coding, labelling, and secondary packaging of pasteurised milk.
4
Curd, Yoghurt and Lassi Production Line
A complete production line for hygienic preparation, fermentation, blending, filling, and cooling of curd, yoghurt, lassi, and buttermilk
5
Paneer and Chhana Production Line
A hygienic production line for efficient milk coagulation, whey separation, pressing, chilling, cutting, and packaging of paneer and chhana.
6
Cream, Butter and Ghee Production Line
A complete processing line for efficient cream separation, pasteurisation, butter making, and ghee production with controlled heating and filtration.
7
Khoa and Traditional Dairy Products Section
A specialized processing setup for efficient milk concentration, khoa preparation, cooking, mixing, cooling, and forming of traditional dairy products.
8
Milk Powder and Whey Processing Section
A specialized processing system for milk and whey clarification, filtration, concentration, drying, and powder handling
9
CIP and Sanitation System
An automated cleaning and sanitation system designed for hygienic maintenance of tanks, pipelines, pasteurisers, and filling equipment
10
Refrigeration and Cold-Chain System
A comprehensive refrigeration system designed to maintain the required temperature for milk, dairy products, and cold storage facilities.
11
Utilities and Support Systems
A comprehensive support infrastructure providing steam, hot water, treated water, refrigeration, compressed air, and electrical power for smooth plant operations.
Dairy Product Processing Lines
Flexible lines for multiple dairy products, from fresh milk processing to frozen desserts.
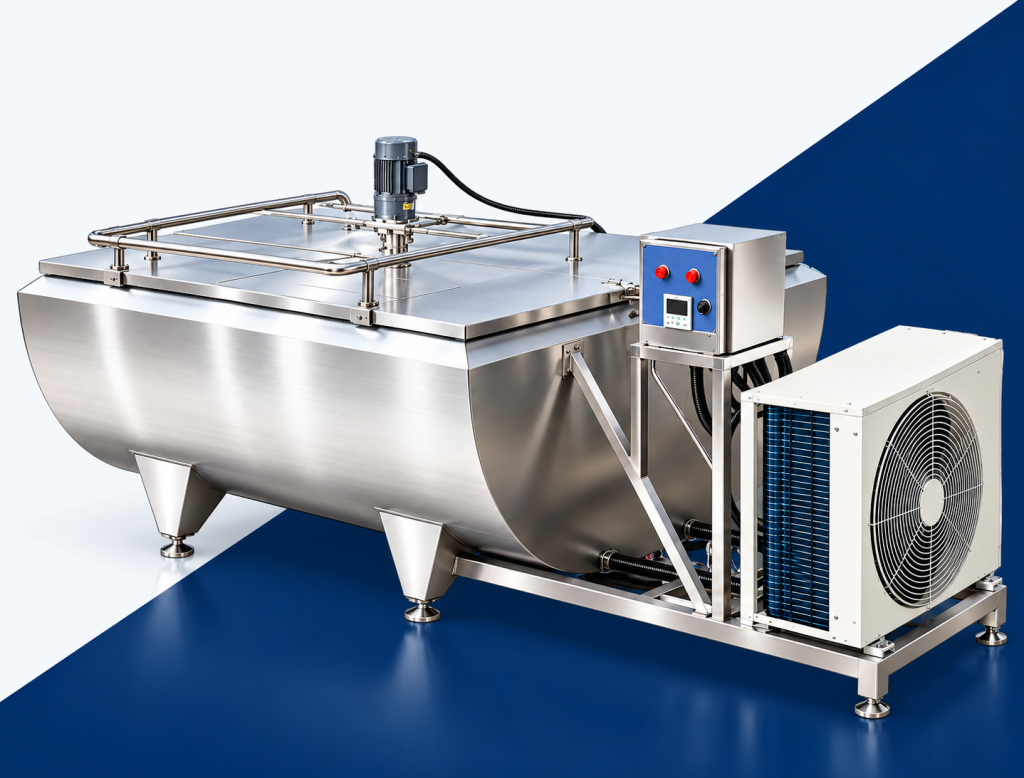
Bulk Milk Cooling Tanks
Suitable for cooling / storage of fresh milk at 4°C. Available in capacities from 200–5,000 litres of milk storage. These can be offered in conventional electrical or solar-powered units, which can switch to grid electricity as a backup in case of low thermal energy levels.
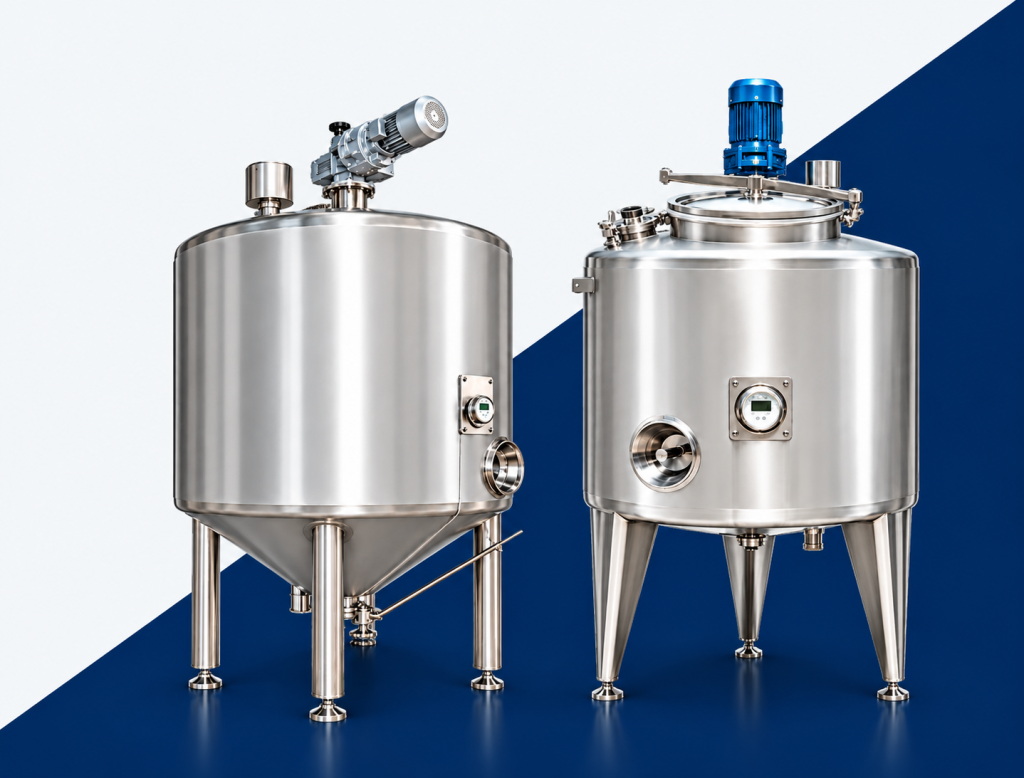
Milk Collection / Storage / Heating Blending Tank
Suitable to store / heat / chill / blend milk and other value-added milk products. Available in single / double / triple layers with jacketing / insulation and stirrer, for 200–10,000 litre volume capacity in SS304/316L.
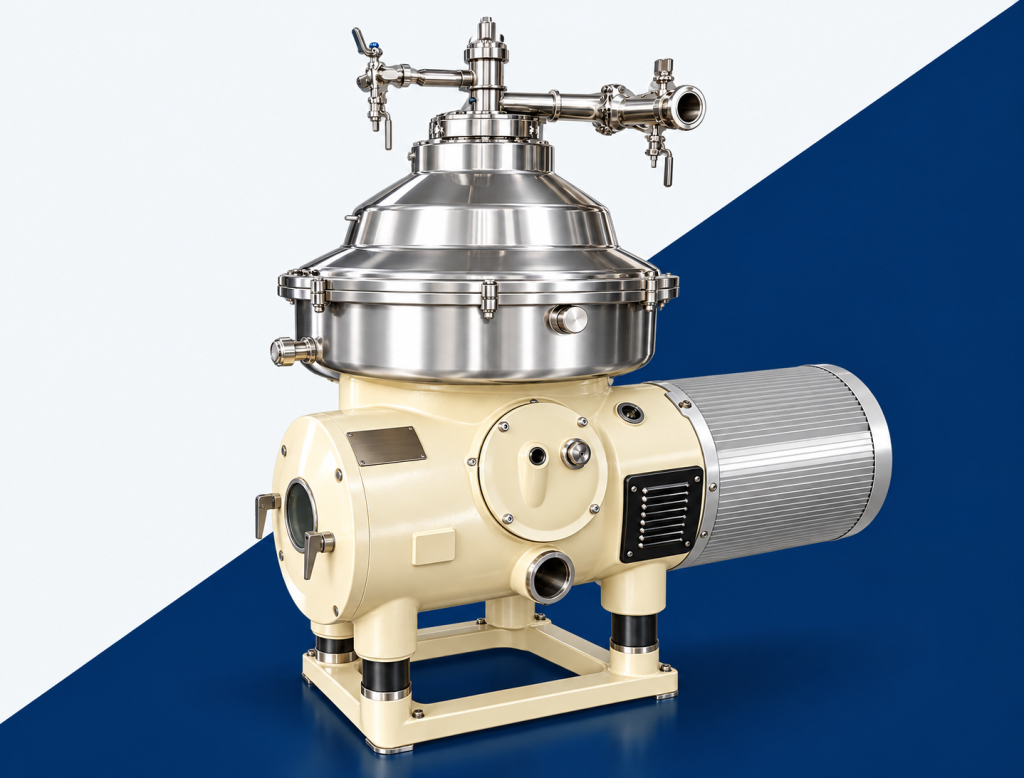
Cream Separator
Suitable for separating fat / cream from milk for standardization. Available in 200–5,000 L/h capacities.
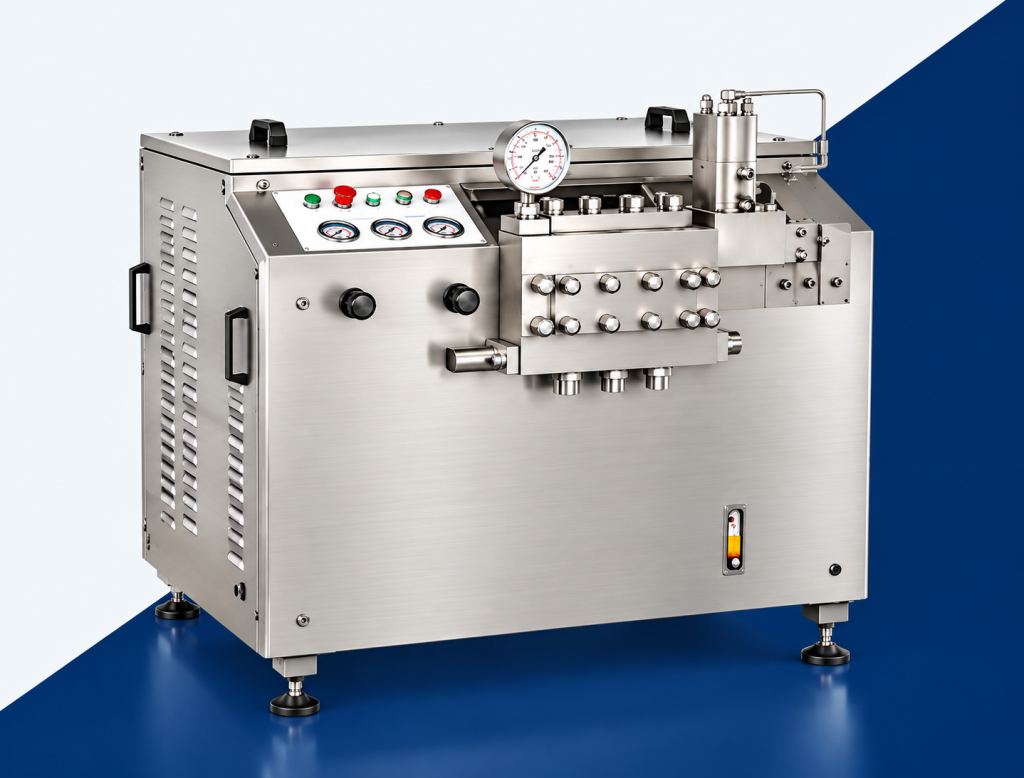
Homogenizer
Suitable to homogenize milk / ice cream mix / yoghurt, etc. to an even consistency. Available from 200–5,000 LPH.
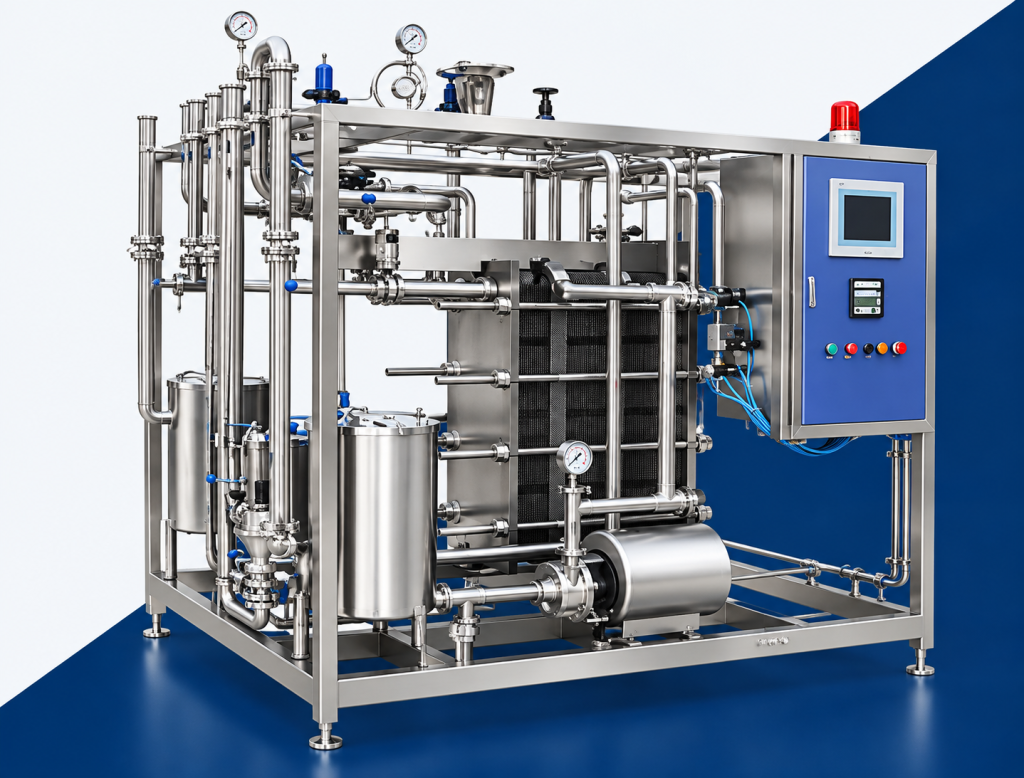
Pasteurizer
Suitable to pasteurize milk / skimmed milk / butter / whey / cream. Incorporates automation for steam / auto diversion / regeneration and chilling. Available in capacities from 200–5,000 L/h.
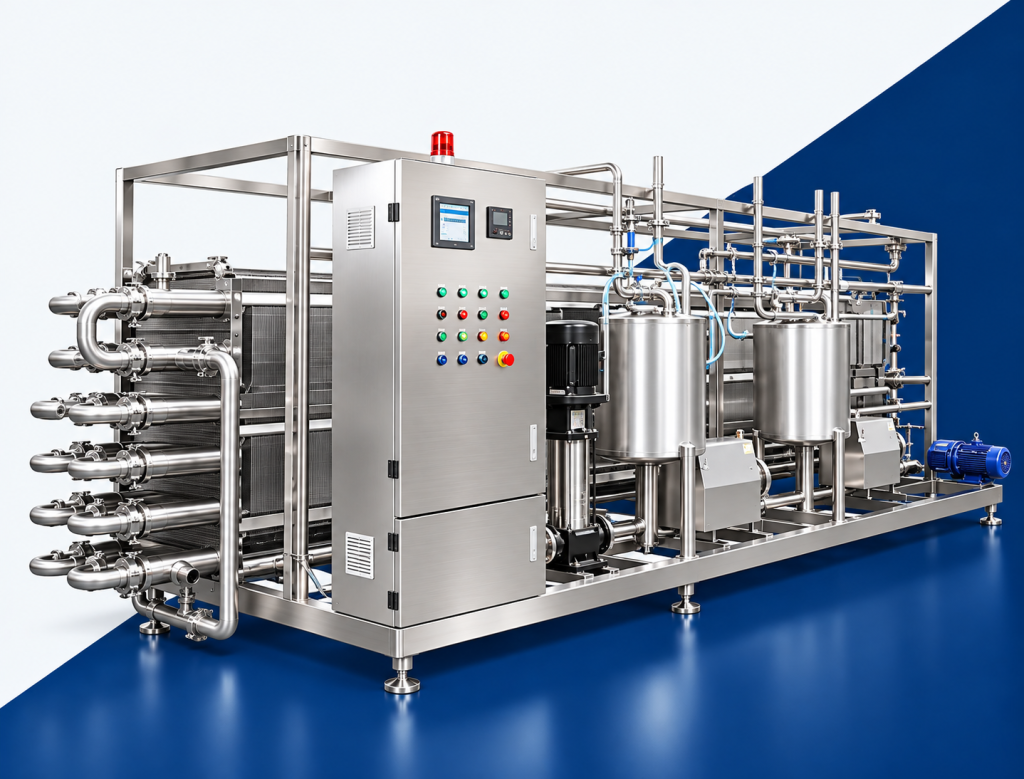
UHT Sterilizer
Suitable to sterilize milk for UHT / aseptic milk for long shelf life. Available in capacities from 200–5,000 L/h.
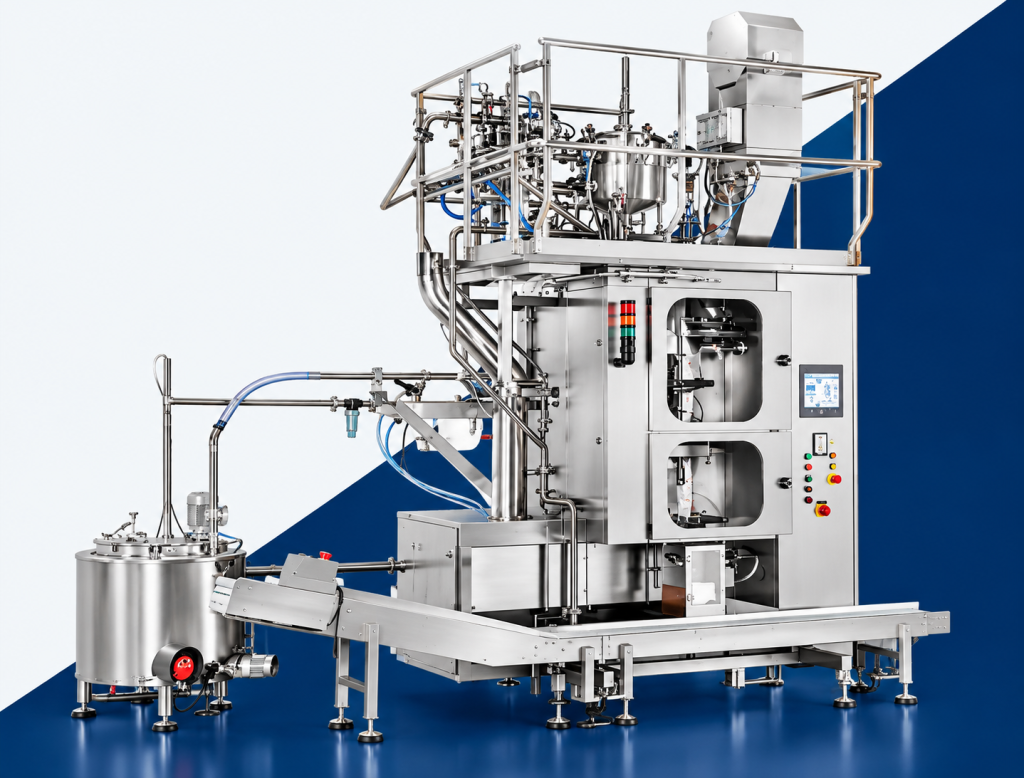
UHT/Aseptic Pouch Packaging Machine
Suitable for packing pasteurized / UHT milk. Available in capacities from 1,000–5,000 pouches per hour.
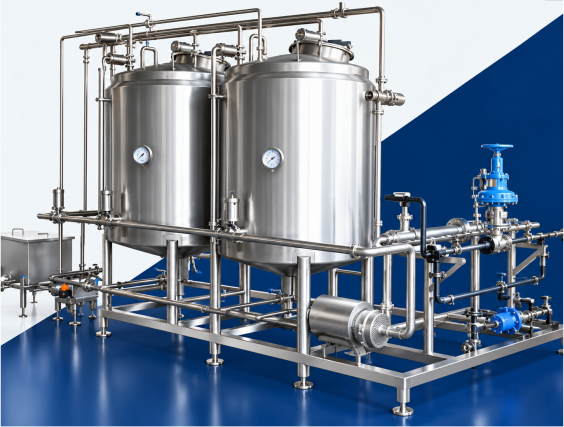
CIP System (Clean-In-Place)
CIP systems are required for thorough cleaning of various equipment / pipelines installed in dairy / food or beverage industries. The system helps reduce microbial growth in the product and enhances product quality. CIP systems are available in 2/3 tank systems in semi-automatic / automatic design models.
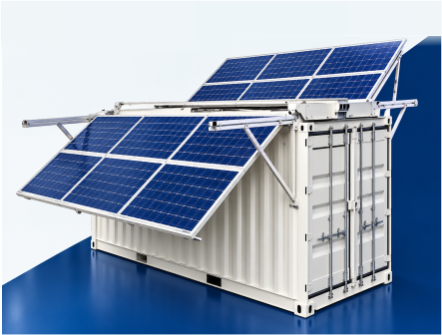
Cold Store
Suitable for cold storage of raw / intermediate / final milk products in a temperature range between 2–15°C. These units can be set up in off-grid areas or can be designed to work on solar power, with switching to grid electricity as a backup in case of low thermal energy levels. These can be designed and/or offered for capacities ranging between 10–50 MT cold store capacity.
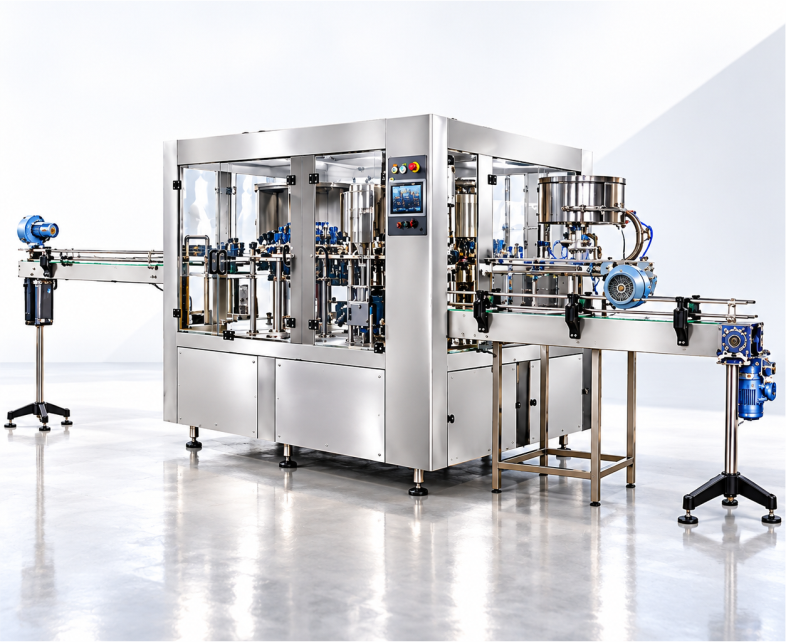
Mechanical and Electronic Grading
Typical capacity range: 1,000–10,000 bottles/hour
Packaging lines can be configured for fresh milk, yoghurt and flavoured milk in bottles, jars, cups and cans, with automatic rinsing, filling, capping and sealing options.
- Automatic bottle / can filling
- Glass bottle cap sealing
- Cup filling and sealing
- Automatic rinser-filler-capper
Cold Storage for Post-Harvest Loss Reduction
Biomass and solar powered cold rooms can be added for farm-level storage, pre-cooling, ripening and perishable produce handling.
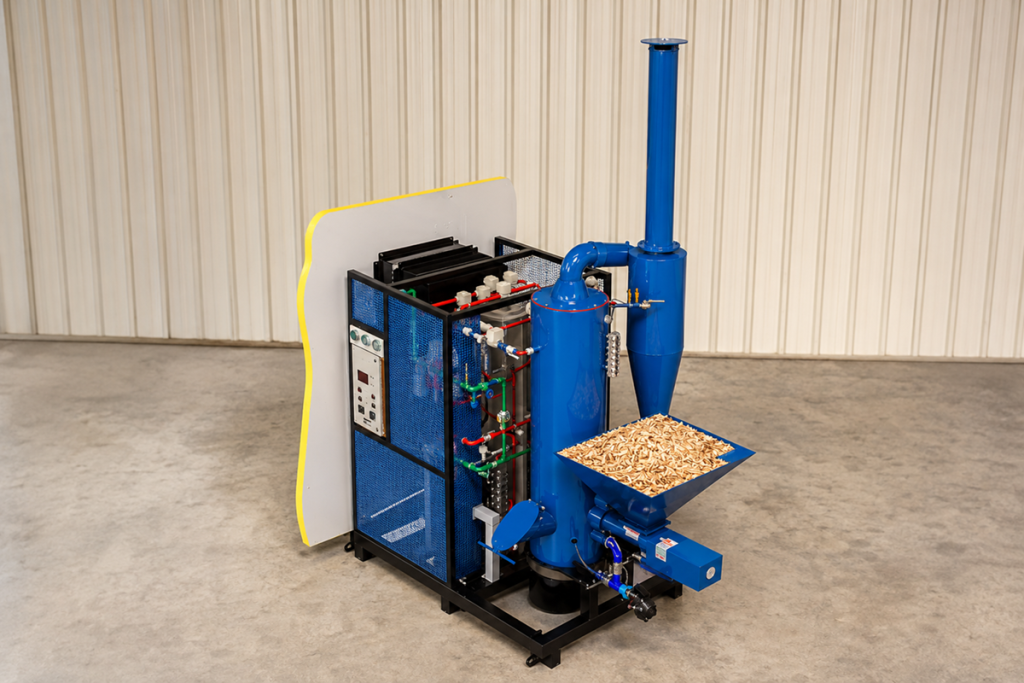
Biomass Powered Cold Room
Available for 10-40 MT capacity with temperature range from +2°C to +25°C and humidity range from 65% to 95%.
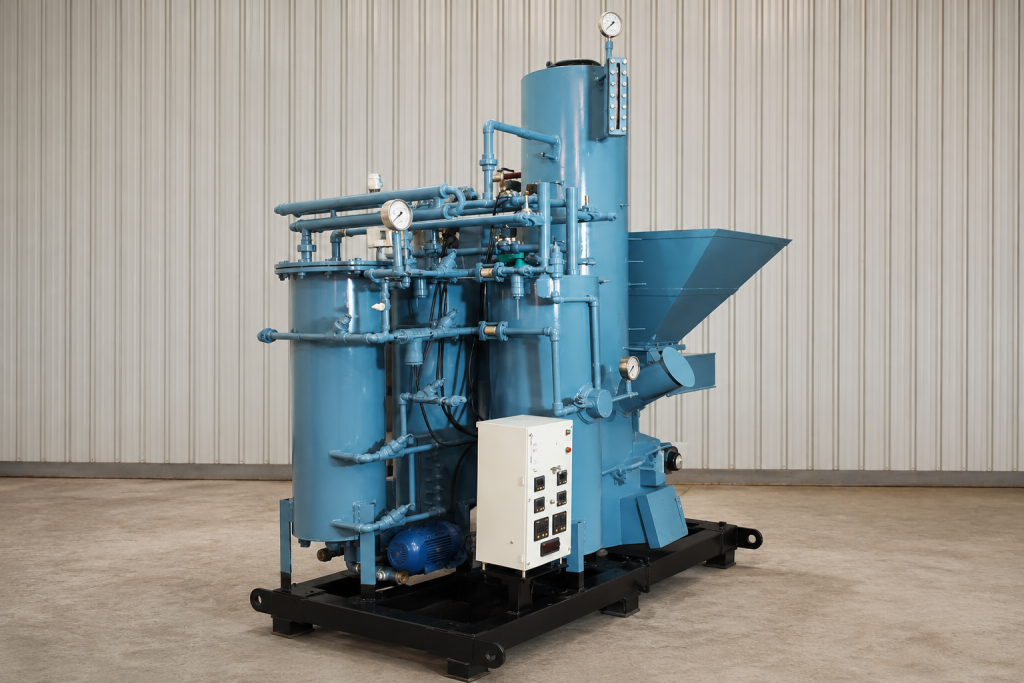
Solar Hybrid Cold Store
Thermal energy storage based cold stores for 5-20 MT capacity with solar backup and optional grid support.
Enquiry Form
Have questions or want to learn more about our services and
solutions? Fill out the form below, and one of our experts will get back
to you promptly.
Form submitted successfully